Industrial Intelligent Pallet Storage Systems
Factory-direct automated racking, radio shuttles, and robotic material handling solutions certified for UK structural and safety compliance.
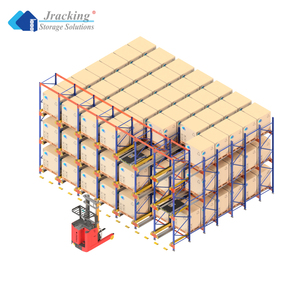
Four-Way Radio Shuttle Automated Pallet Rack System
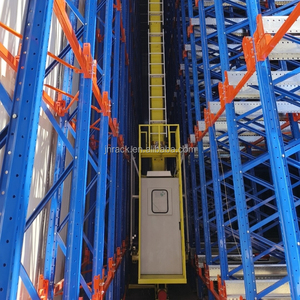
Intelligent ASRS Chain Pallet Conveyor System
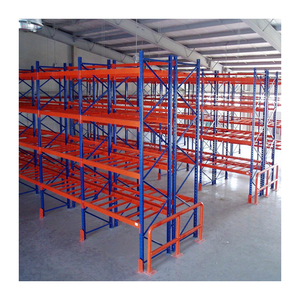
Compact Pallet Shuttle High-Density Racking System
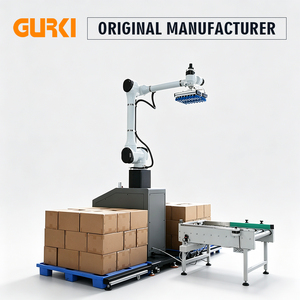
High-Speed Full Automatic Robotic Palletizing System
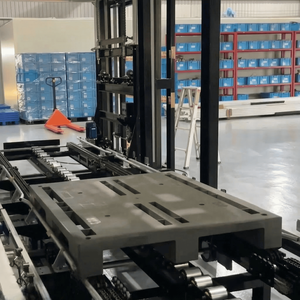
90-Degree Heavy-Duty Pallet Transfer Conveyor Unit
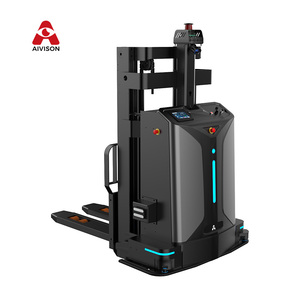
Autonomous Mobile Robot (AMR) Pallet Forklift AGV
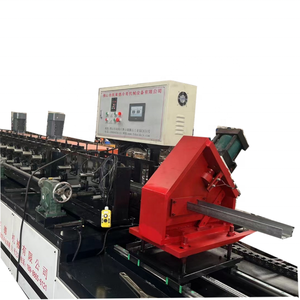
High-Productivity Motorized Stacking Pallet Rack System
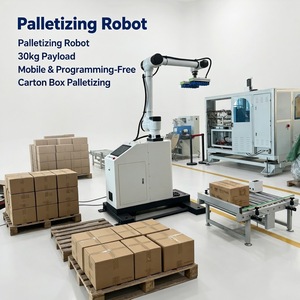
AI-Driven Pallet Pattern & Load Optimization Robot
Solving London's Urban Logistics & Warehouse Footprint Bottlenecks
Logistics directors, warehouse operators, and industrial real estate asset managers across Greater London face an unprecedented structural challenge: prime industrial rents in key hubs like Park Royal, Heathrow, Enfield, and the Thames Gateway corridor have escalated to record highs (£25 to £35+ per sq. ft.). Compounded by stringent municipal planning constraints, low clear-height legacy brownfield facilities, and the rapid expansion of same-day micro-fulfillment, expanding horizontally is no longer financially or operationally viable.
As a premier direct manufacturer of intelligent pallet storage systems serving London, our engineering division delivers structural steel racking, automated radio shuttle technology, and automated storage and retrieval systems (ASRS) specifically optimized to unlock vertical cube space. By replacing legacy wide-aisle selective racking with four-way automated pallet shuttles and autonomous mobile robots (AMRs), London enterprises can achieve up to 85% volumetric space utilization while drastically reducing operational labor overhead.
In a standard 3,000 m² London distribution warehouse, traditional selective racking yields approximately 2,400 pallet positions with 3.5m aisles for reach trucks. Upgrading to an Automated 4-Way Radio Shuttle Racking System compresses aisle width to shuttle transfer points, expanding capacity to 4,850+ pallet positions within the identical structural envelope—effectively halving the rental cost per stored pallet per annum.
Engineering Principles of Our Automated Racking Platforms
Built using high-tensile European standard steel (Q355B / S355 grade) with precision-machined guide rails and intelligent WCS integration.
High-Tensile Structural Steel Frame
Fabricated from cold-rolled S355/Q355B structural steel profiles engineered to exceed UK SEMA and BS EN 15512 static design codes. Upright frames feature continuous teardrop or upright slots for effortless beam height adjustments in 75mm increments.
4-Way Shuttle Kinematics
Our ultra-slim 4-Way Radio Shuttles traverse both longitudinal channels and transverse aisles. Powered by quick-charge Lithium Iron Phosphate (LiFePO4) battery packs, they feature automatic cross-aisle changing for uninterrupted 24/7 dark-warehouse operations.
PLC & WMS Software Connectivity
Seamless REST API and OPC UA industrial communication protocols bridge factory-floor PLCs (Siemens S7-1500 series) with enterprise management software including SAP EWM, Manhattan Associates, Oracle WMS, and bespoke UK cloud platforms.
Storage Technology Performance & Selection Matrix
Comparative engineering metrics to assist London warehouse operations managers in selecting optimal pallet handling architectures.
| Storage System Architecture | Volumetric Efficiency | Selectivity & Access | Floor Space Reduction | WMS Automation Integration | Ideal London Industry Use Case |
|---|---|---|---|---|---|
| 4-Way Radio Shuttle Racking | 85% - 90% | Batch / Channel Selective | Up to 60% | Full (WCS Driven) | Cold Storage, FMCG, Beverage Distribution |
| Crane-Based Automated ASRS | 90% - 95% | 100% Automatic | Up to 70% | Native Enterprise ASRS | High-Bay E-Commerce Hubs (15m+ Height) |
| Autonomous Mobile Robot (AMR/AGV) | 70% - 80% | 100% Dynamic | Up to 40% | Fleet Management System | Third-Party Logistics (3PL), Micro-Fulfillment |
| Traditional Selective Pallet Racking | 40% - 50% | 100% Manual Access | 0% (Baseline) | Barcode Scan Only | Low SKU Volume, Low Rent Regional Depots |
Targeted Engineering Solutions across London Industrial Zones
1. Park Royal & West London Micro-Fulfillment
Serving the UK's largest food manufacturing and catering hub (Park Royal), our stainless steel and hot-dip galvanized radio shuttle racks operate reliably in sub-zero freezer environments (-25°C). High-density channels prevent thermal loss by packing frozen inventory tightly, reducing refrigeration energy consumption by up to 35%.
2. Heathrow Logistics Corridor (M4 / M25 Air Freight)
High-turnover freight forwarders surrounding Heathrow Airport require rapid pallet cycle times. Our Intelligent Chain & Roller Conveyor Systems coupled with heavy-duty transfer units handle standard UK (1200x1000mm) and Euro (1200x800mm) pallets instantly, providing seamless air-cargo ULD pallet breakdown and rack buffering.
3. Thames Gateway & Dagenham High-Bay ASRS
In newly developed logistics parks along the Thames Estuary, land developers utilize vertical clear heights exceeding 18 meters. We design and manufacture clad-rack warehouse structures and automated stacker crane ASRS systems, anchoring heavy structural posts to engineered concrete slabs engineered for high floor-load ratings.
4. East London & Urban Last-Mile Logistics
Converting historic brownfield industrial units in Enfield or Dartford into automated e-commerce hubs. Our Autonomous Mobile Robot (AMR) Forklift AGVs navigate narrow doorways and low-overhead clearance zones without requiring permanent floor-mounted magnetic tracks, providing flexible deployment for leased premises.
Why Global Procurement Directors Choose Our Factory
From raw steel coil processing to robotically welded beams and automated powder coating—complete control over product quality and delivery timelines.
Automated Production Lines
Our state-of-the-art manufacturing facility houses 26 continuous cold-roll forming lines, automated laser tube cutters, and Panasonic robotic welding cells, ensuring tight dimensional tolerances across all upright profiles and beams.
Strict Quality Control & Testing
Every batch of raw steel undergoes mechanical tensile strength testing, weld ultrasonic inspection, and epoxy coating thickness verification. All rack structural designs are verified via Finite Element Analysis (FEA) software.
Export Packaging & Logistics Support
Components are bundled with corner protection, protective film, and heavy-duty steel strapping. Direct sea-freight shipping routes from our factory to major UK ports (Felixstowe, London Gateway, Southampton) ensure hassle-free delivery.
Frequently Asked Questions for London & UK Buyers
Technical, structural, and commercial guidance for engineering consultants, warehouse owners, and project managers.
Optimize Your London Warehouse Volume Today
Send us your warehouse structural CAD drawings, building dimensions, and pallet storage requirements. Our senior logistics system engineers will deliver a comprehensive 3D layout plan and factory-direct quotation within 24 hours.