Pharmaceutical Storage Racking Product Showcase
Engineered OEM/ODM solutions tailored for raw material cleanrooms, automated quarantine distribution, and temperature-sensitive storage.
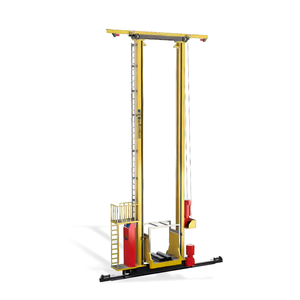
Intelligent Miniload Stacker Crane Pallet Racking
Fully automated AS/RS shuttle storage ideal for batch-controlled pharmaceutical raw materials and cleanroom totes.
Contact Us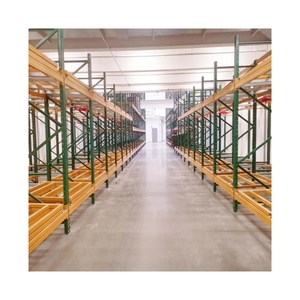
Push Back Pallet Racking System with Precision Guide Rail
High-density LIFO storage designed for pharmaceutical batch tracking and cold-chain room space optimization.
Contact Us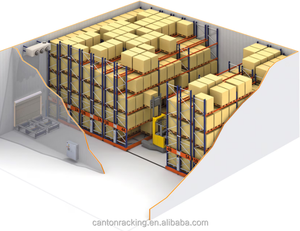
Compaction Mobile Pallet Racking System
Motorized mobile bases that eliminate fixed aisles, maximizing cold storage efficiency for biopharmaceuticals.
Contact Us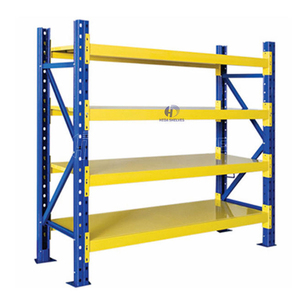
Selective Heavy Duty Warehouse Pallet Racking
Provides 100% SKU selectivity for diverse pharmaceutical finished goods, compliance testing, and swift picking.
Contact Us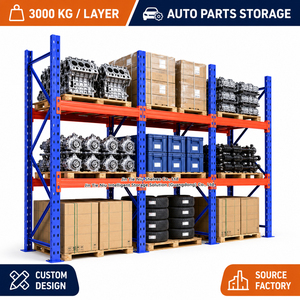
Custom OEM Heavy Duty Selective Racking (200-4000KG)
Fully customizable beam height and load capacity configured for pharmaceutical barrel and drum storage.
Contact Us
Heavy Duty 5-Layer Drive-In Pallet Storage Rack
Maximizes volume for high-quantity single SKU pharmaceutical products under strict ambient climate control.
Contact Us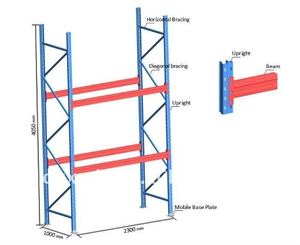
High-Density Single Deep Metal Industrial Racking
Engineered steel uprights with anti-corrosive powder finish designed for strict cleanroom sanitation standards.
Contact Us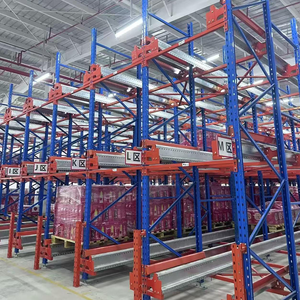
Automated Two-Way Radio Shuttle Pallet Racking
Corrosion-resistant shuttle cart racking system providing automated deep-lane storage for vaccine cold stores.
Contact Us1. Pharmaceutical Storage Architecture: Regulatory Standards & Material Selection
In modern pharmaceutical warehousing, pallet racking systems are far more than structural steel frame assemblies—they form the core infrastructure governing Current Good Manufacturing Practice (cGMP) compliance, Good Distribution Practice (GDP), and FDA Title 21 CFR Part 211 mandates. Choosing the right OEM/ODM pharmaceutical pallet racking factory requires rigorous evaluation of metallurgical purity, surface finishing technology, and structural cleanability.
Pharmaceutical products—ranging from Active Pharmaceutical Ingredients (APIs) to biologic cold-chain vaccines—require storage environments that prevent cross-contamination, resist chemical washing agents, and maintain structural integrity across extreme temperature gradients (from ambient +25°C down to sub-zero -30°C freezer facilities).
Cleanroom ISO 14644 Integrity
Sealed tubular upright profiles and crevice-free beam connection welds prevent dust accumulation and particle shedding in ISO Class 7/8 environments.
Antimicrobial Powder Coatings
Electrostatically applied epoxy-polyester coatings embedded with silver-ion agents to continuously inhibit bacterial growth and mold colonization.
Sub-Zero Ductility Steel
Specialized Q355B low-alloy steel certified for high impact resistance at -30°C without experiencing cold embrittlement or structural fatigue.
2. OEM/ODM Engineering Customization for Pharma Warehouses
Off-the-shelf industrial shelving rarely aligns with pharmaceutical spatial logistics. Specialized OEM/ODM racking factories provide custom structural calculations using Finite Element Analysis (FEA) to verify beam deflection ratios under dynamic load stresses while ensuring compatibility with automated material handling equipment.
Key custom engineering directives for pharmaceutical procurement teams include:
- First-Expiry, First-Out (FEFO) Layout Integration: Configuring push back racking and two-way radio shuttle systems to ensure exact lot number tracking and seamless expiration-date inventory rotation.
- Seismic & Dynamic Load Resistance: Structural rack calculation complying with R-factor dynamic specs and ASCE 7 seismic zone regulations, protecting millions of dollars in fragile glass vial inventory.
- Cleanable Floor Anchor System: Stainless steel expansion anchors and flush-mounted base plates designed with smooth rubber perimeter gaskets to prevent moisture trapping during chemical floor scrubbing.
For high-density logistics projects, linking your racking configuration directly to specialized pallet types is crucial. For instance, pairing heavy-duty rack frames with Galvanized Steel Pallets or light-weight Aluminum Pallets guarantees sterile contact surfaces and maximum load uniformity.
3. Technical System Matrix: Selecting the Right Pharma Storage Racking
Selecting the correct OEM configuration depends directly on SKU diversity, cold-room operational costs, and inventory rotation speeds. The matrix below outlines structural metrics for key systems:
| Racking Type | Storage Density | FEFO / FIFO Compliance | Cleanroom Compatibility | Cold Chain Efficiency | Optimal Pharma Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | Standard (40-50%) | 100% Selective (FIFO) | High (Easy Washdown) | Moderate | Quarantine Zones, High SKU Finished Goods |
| Radio Shuttle Racking | Ultra-High (85%+) | Programmable FIFO/LIFO | Excellent (No Forklift Dust) | Maximum (Cold Air Flow) | Vaccine Deep Freezers, Bulk APIs |
| Push Back Racking | High (65-75%) | LIFO (Per Lane) | Good | High | Batch-Based Intermediate Packaging |
| VNA (Very Narrow Aisle) | High (70-80%) | 100% Selective | High | Good | High-Bay Vertical Distribution Centers |
| Mezzanine Platform Rack | Vertical Double/Triple | Manual Picking FIFO | Medium to High | Standard Ambient | Small-Pack Medicinal Goods, E-Commerce |
4. Future Procurement & Technological Trends in Pharmaceutical Storage
The global pharmaceutical supply chain is undergoing rapid transformation driven by automation, sustainability mandates, and stringent traceability laws. Procurement teams sourcing from OEM/ODM racking factories must factor in these four upcoming industry shifts:
1. Dark Warehouse AS/RS Integration
Fully automated, unmanned warehouses operating in total darkness to eliminate human contamination and reduce HVAC energy overhead by up to 40%.
2. IoT & RFID Sensor Embedded Racking
Smart rack beams integrated with micro-temperature sensors and RFID tracking to monitor cold-chain compliance at individual pallet locations in real-time.
3. Zero-Microbial Hygienic Coatings
Next-generation nanotech ceramic-epoxy coatings that naturally shed water, resist harsh sterilization chemicals (Vaporized Hydrogen Peroxide), and prevent bio-film buildup.
When upgrading your facility to support automated guided vehicles (AGVs) or radio shuttles, integrating standardized pallet media like heavy-duty HDPE Plastic Pallets ensures reliable dimensional consistency, preventing shuttle cart jamming and sensor reading errors.
5. Why Partner with Our OEM/ODM Racking Manufacturing Base?
Our state-of-the-art production complex in Shandong, China, provides global pharmaceutical brands, hospital supply chains, and third-party logistics (3PL) providers with direct factory access to heavy-duty storage infrastructure. By consolidating design, cold-roll forming, robotic welding, and coating under one roof, we eliminate intermediary markups while upholding rigorous European (FEM 10.2.02) and American (RMI) engineering benchmarks.
- Direct Steel Traceability: Sourcing prime structural steel coils with mill test certificates (MTC) verifying yield strength and chemical composition.
- Automated Laser Cutting & Robotic Welding: High-precision robot arms execute continuous, smooth welds with zero spatter, ensuring clean surface finishes suitable for pharma washdowns.
- Comprehensive OEM Engineering Support: Full CAD design service, 3D BIM modeling, dynamic FEA structural reporting, and remote installation guidance provided for every order.
- Export-Ready Logistics Packaging: Uprights and beams packaged with heavy-duty plastic wrapping, steel strapping, and wooden skid blocks to protect finished coatings during ocean transport.
6. Technical Buyer FAQ: OEM/ODM Pharmaceutical Pallet Racking
Engineering Your Pharmaceutical Storage Infrastructure
Partner directly with a certified OEM/ODM factory. Contact our senior structural engineers today to receive CAD layout drawings, load calculations, and competitive direct-factory pricing.
Contact Us