Featured Heavy-Duty Racking & Pallet Systems
Engineering-grade storage configurations engineered for industrial logistics, cold storage, and high-density warehouse transit nodes.
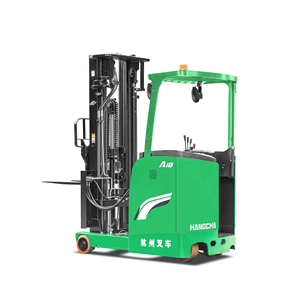
1.5 Ton 2 Ton 2.5 Ton High Lift Reach Truck 3m-10m For Narrow Aisle Warehouse Pallet Storage
Inquire Now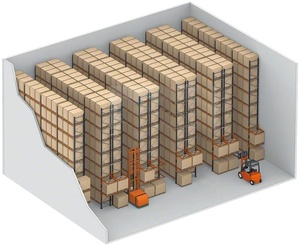
URGO Very Narrow Aisle Pallet Rack / VNA Racking System High Density Storage
Inquire Now
3 Layer Heavy-Duty Metal Storage Rack Steel Pallet Rack Wholesale for Warehouses
Inquire Now
Separate Channel Access 5 Layer Metal Pallet Stacking Frame Warehouse Rack
Inquire Now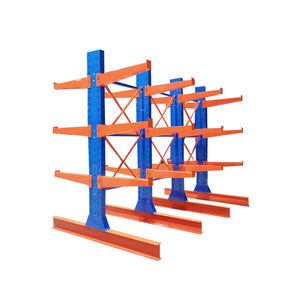
Powder Coated Cantilever Racking System - Heavy Duty Warehouse Storage Shelves
Inquire Now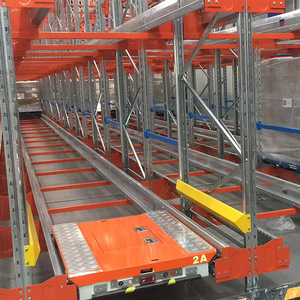
Jracking CE-Certified Radio Shuttle Rack System Space-Saving Automated Storage
Inquire Now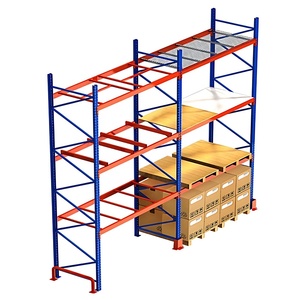
Heavy Duty Shelving System Multilayer Cross Beam Storage Rack CE/ISO Certified
Inquire Now
High Quality Warehouse Heavy Duty Pallet Racking Black Rack & Drum System
Inquire Now1. Technical Overview: Block Stacking Racking Systems vs. Fixed Structural Racking
In modern industrial logistics, floor-space optimization and volumetric store density represent critical drivers of operational profitability. As an established OEM/ODM Block Stacking Racking System Supplier, IronMax Storage Solutions Co., Ltd. delivers engineered racking and modular stacking frameworks tailored for high-density warehouse hubs, cold chain distribution logistics, and automated transit centers worldwide. Understanding the mechanical differences between traditional fixed selective racking and modular block stacking racking systems is crucial for supply chain directors and warehouse operations engineers.
Block stacking racking systems—often realized through modular pallet stacking frames, portable nestable post racks, or high-density drive-in and shuttle configurations—enable operators to stack unit loads directly on top of one another safely without causing product crush or structural deformation. Traditional block stacking (placing bare pallets directly on top of lower goods) is strictly limited by packaging crush strength and localized load limits. By integrating engineered heavy-duty steel stacking frames, loads are transmitted entirely through cold-rolled steel posts directly to the floor slab, creating a modular, vertical storage system that requires zero permanent building anchorages.
Furthermore, for facilities operating in rented properties or multi-tenant logistics parks, permanent anchored selective racks represent significant capital expenditure and civil compliance hurdles. Modular block stacking racking offers complete dynamic flexibility: when seasonal demand surges, stacking frames can be rapidly configured into dense storage blocks; when inventory clears, the frames fold flat or nest compactly, clearing thousands of square meters of floor space for general cross-docking operations.
2. Structural Integrity, FEA Metallurgy, and Load Mechanics
The engineering philosophy at IronMax relies on advanced Finite Element Analysis (FEA) and strict compliance with international structural codes including EN 15512 (European Racking Code), RMI (Rack Manufacturers Institute), and ISO 9001 quality management protocols. Every OEM/ODM custom racking profile undergoes rigorous dynamic stress testing to guarantee structural safety under static loads, operational impact, and seismic accelerations.
Metallurgical Specifications & Profile Selection
Primary load-bearing components—such as upright columns, heavy-duty box beams, cantilever arms, and stacking frame channels—are cold-roll formed from premium-grade Q235B and high-yield Q355B structural steel coils. Q355B steel offers a minimum yield strength of 355 MPa, providing superior load-to-weight ratios compared to standard structural mild steels. This high tensile resistance ensures minimal cross-sectional beam deflection even under maximum load ratings ranging from 500 kg to 5,000 kg per level.
Finite Element Analysis (FEA)
Computerized stress mapping simulates maximum vertical point loads, corner post buckling, and sway torsional forces. FEA validation guarantees safety factors between 1.5x and 2.0x standard load ratings.
Deflection Threshold (L/200)
All horizontal cross-beams and stacking frames adhere to strict L/200 deflection criteria. Under total capacity loading, maximum beam sagging is constrained within 1/200th of the clear beam span.
Surface Pre-Treatment & Coating
Components undergo an 8-stage chemical wash, phosphating, and automatic electro-static epoxy powder coating cured at 200°C, providing exceptional impact, scratch, and corrosion resistance.
Seismic Resistance & Dynamic Base Locking Mechanisms
For heavy industrial installations situated in active seismic zones, standard block stacking requires precision structural interlocking. IronMax OEM design engineers incorporate interlocking male-to-female post caps and cup-shaped baseplates into stackable frames. These heavy-gauge steel alignment cups automatically guide forklift tines during multi-tier placement while mechanically preventing horizontal sliding or dynamic dislodgement during sudden seismic shifts or accidental forklift bump impacts.
3. Comparative Matrix: High-Density Warehouse Storage Technologies
Selecting the optimal warehouse racking system requires evaluating trade-offs between capital investment, storage density, individual SKU selectivity, and material handling equipment compatibility. The matrix below provides an engineering comparison of primary industrial storage systems manufactured by IronMax.
| Racking System Type | Storage Density | SKU Selectivity | Load Capacity / Tier | Ideal Goods & Applications |
|---|---|---|---|---|
| Modular Block Stacking Frames | High (80-85%) | Medium (Per Stack) | 1,000 kg – 2,500 kg | Seasonal inventory, fragile bulk boxed items, rented facilities, rapid transit hubs. |
| Selective Pallet Racking | Standard (50-60%) | 100% Immediate | 500 kg – 4,000 kg | High SKU counts, fast-moving consumer goods (FMCG), general distribution. |
| Very Narrow Aisle (VNA) | Very High (85-90%) | 100% Immediate | 1,000 kg – 2,000 kg | High-bay warehouses, expensive urban land, specialized VNA reach truck operation. |
| Radio Shuttle Racking | Maximum (90-95%) | Low (Lane Selective) | 1,000 kg – 1,500 kg | Cold storage freezers, food & beverage bulk channels, high-throughput automated logistics. |
| Drive-In Pallet Racking | High (75-85%) | Low (LIFO Flow) | 1,000 kg – 2,000 kg | Uniform bulk SKUs, cold storage rooms, low-rotation heavy palette inventory. |
| Cantilever Racking Systems | Medium (Custom) | 100% Open Access | 500 kg – 3,000 kg/Arm | Long, oversized, or irregular loads: steel pipes, timber planks, plastic extrusions. |
4. Future Procurement Trends in Industrial Storage Architecture (2025–2030)
As global supply chains shift toward automated warehousing, localized distribution hubs, and strict ESG (Environmental, Social, and Governance) compliance, procurement strategies for block stacking and industrial racking are evolving rapidly. B2B buyers must anticipate several key technological shifts when sourcing racking systems over the coming decade.
A. Integration with Autonomous Mobile Robots (AMRs) & AGVs
Traditional pallet racking was designed exclusively around human-driven reach trucks and counterbalance forklifts. Modern supply chain projects increasingly integrate AGVs (Automated Guided Vehicles) and autonomous forklifts. This transition demands higher manufacturing precision: rack tolerances, post straightness, and beam deflection must meet ISO 286 precision grades to prevent robotic positioning errors. Block stacking frames designed by IronMax feature widened self-centering guide entries that accommodate AMR tine alignment tolerances down to millimeter accuracy.
B. Smart Racking & IoT Weight-Monitoring Sensors
Future-ready block stacking and heavy-duty beam racks are transitioning into smart infrastructure nodes. By embedding micro-strain gauges and wireless IoT load sensors into primary cross beams and stacking frame legs, facility managers can monitor real-time weight distribution via cloud dashboards. These sensors detect localized structural overloading, asymmetrical load balances, and subtle frame tilt, triggering automated safety alerts before structural fatigue or localized beam deformation can occur.
C. Cold Chain Eco-Coatings & Green Galvanizing
With cold-storage energy costs escalating globally, maximizing cold-room volumetric density via compact radio shuttle racks and stackable pallet frames is paramount. Furthermore, environmental regulations are phasing out volatile organic compound (VOC) heavy paints. High-grade hot-dip galvanizing (HDG) and zero-emission thermosetting powder coating solutions are becoming standard procurement mandates. IronMax galvanized systems provide hot-dip zinc coverage exceeding 65–85 μm thickness, ensuring 25+ years of rust-free performance in sub-zero freezer environments operating as low as -30°C.
5. Enterprise OEM/ODM Manufacturing Capabilities & Engineering Workflow
As a dedicated Chinese manufacturing leader based in Jining, Shandong Province, IronMax Storage Solutions Co., Ltd. operates a vertically integrated production facility encompassing over 120 skilled engineers, certified welders, and production specialists. We specialize in converting client warehouse blueprints and operational parameters into highly optimized physical storage hardware.
1. Custom Layout & CAD Design
Send us your warehouse CAD drawings, building clear heights, forklift specs, and pallet dimensions. Our structural design team generates optimized 2D layout options and 3D isometric BIM models within 24 hours.
2. Precision CNC & Automated Roll Forming
Utilizing high-speed multi-stage continuous roll-forming lines, cold-rolled steel profiles are punched, notched, and shaped with sub-millimeter pitch accuracy, guaranteeing seamless on-site boltless assembly.
3. Export Bundling & Global Shipping
Uprights and beams are bundled with protective edge guards, steel strapping, and heavy polythene wrapping. Container loading is engineered to prevent coating abrasions and maximize sea freight cube utilization.
6. Frequently Asked Questions (FAQ) for Racking Procurement
Q: What maximum weight capacity can your OEM block stacking frames carry?
Our custom modular pallet stacking frames are engineered to support payloads from 1,000 kg up to 2,500 kg per single tier. When vertically stacked 4 to 6 tiers high, the bottom frame safely transfers cumulative static loads exceeding 10,000 kg to the concrete floor slab. Dynamic FEA calculations and safety factors are calculated individually for each OEM order based on customer pallet dimensions.
Q: How do modular block stacking frames compare to fixed drive-in racking for cold storage?
While drive-in racking provides dedicated permanent lanes, modular block stacking frames offer significantly greater flexibility. Stacking frames require no floor anchor bolts, allowing cold store managers to change seasonal layout configurations freely. When seasonal stock subsides, empty stacking frames dismantle or nest flat, freeing up expansive cold storage spaces for alternative bulk items or maintenance work.
Q: What steel grades and surface finishes do you provide for industrial environments?
We utilize structural cold-rolled steel grades Q235B and Q355B. For dry indoor ambient warehouses, we apply an electro-static epoxy powder coating in custom RAL colors (such as RAL5005 Blue or RAL2004 Orange). For sub-zero freezers, humid chemical environments, or semi-outdoor storage, we provide heavy hot-dip galvanizing (HDG) or pre-galvanized finishes complying with ISO 1461 standards.
Q: Can IronMax design custom racking components to fit our existing third-party racks?
Yes. As a direct OEM/ODM supplier, we frequently manufacture compatible drop-in replacement beams, teardrop uprights, wire mesh decking, and stacking frames tailored to fit existing European, American, or Asian racking profiles. Our engineers work directly from customer-supplied samples or detailed dimensional measurements to ensure perfect fitment.
Q: What structural documentation and installation guidance do you supply with export orders?
Every export project includes structural CAD layout drawings, component elevation details, assembly step-by-step manuals, and certified load capacity plaques. For complex multi-tier mezzanines, automated radio shuttle bays, or VNA racking installations, we offer remote video engineering assistance and on-site supervisor dispatch upon request.
Q: How do you ensure surface finish quality and load integrity prior to dispatch?
Our factory conducts an 8-point Quality Control inspection protocol. Raw coil thickness is verified with ultrasonic gauges; welds undergo magnetic particle or ultrasonic testing; paint adhesion is tested via cross-hatch testing; and sample frames are destructive-load tested on hydraulic press rigs to confirm ultimate failure margins exceed 200% of nominal rating.
Optimize Your Warehouse Density with Certified OEM/ODM Engineers
Whether you require heavy-duty selective pallet racking, custom modular block stacking frames, or automated shuttle systems, our engineering team is ready to analyze your pallet matrix and deliver a turnkey layout design.
Inquire Now